


Automation and cutting technology
TECHTORY Automation GmbH
Ludwig-Winter-Straße 5
77767 Appenweier
| Phone | +49 7805 9589-0 |
| Fax: | +49 7805 9589-50 |
| Email: | info@techtory.de |
Through our comprehensive full service, you benefit from numerous services in the development and realization of customer-specific systems:
Alternatively, we also offer the production and assembly of complete assembly lines and plants according to your individual production and assembly drawings, parts lists, pneumatic and circuit diagrams.
We offer the production and assembly of complete assembly lines and plants according to your individual production and assembly drawings, parts lists, pneumatic diagrams and circuit diagrams.
With our complete service, you benefit not only from efficient assembly production, but also from other services that we can offer in-house:
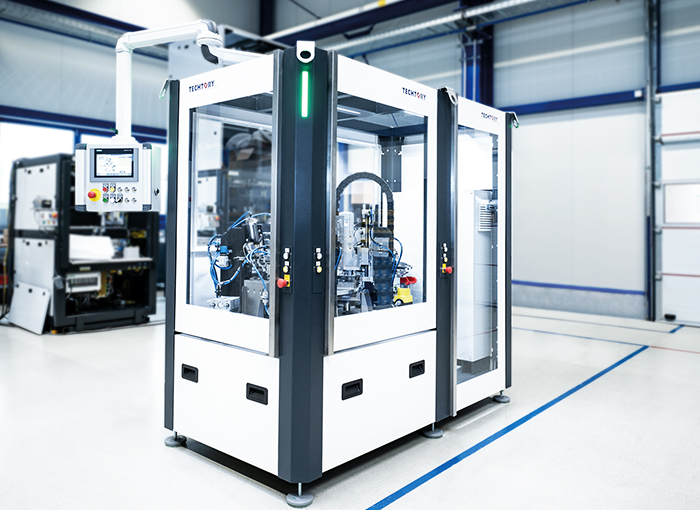
Deburring, brushing, embossing and packing station for sliding blocks
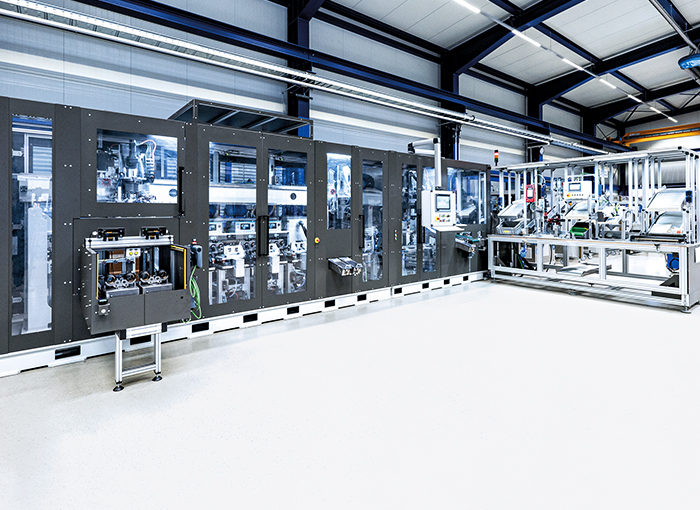
Assembly and testing system for ball valves with a wide range of parts

Assembly and testing system for quick couplings
Deburring, brushing, embossing and packing station for sliding blocks
Assembly and testing system for ball valves with a wide range of parts
Assembly and testing system for quick couplings
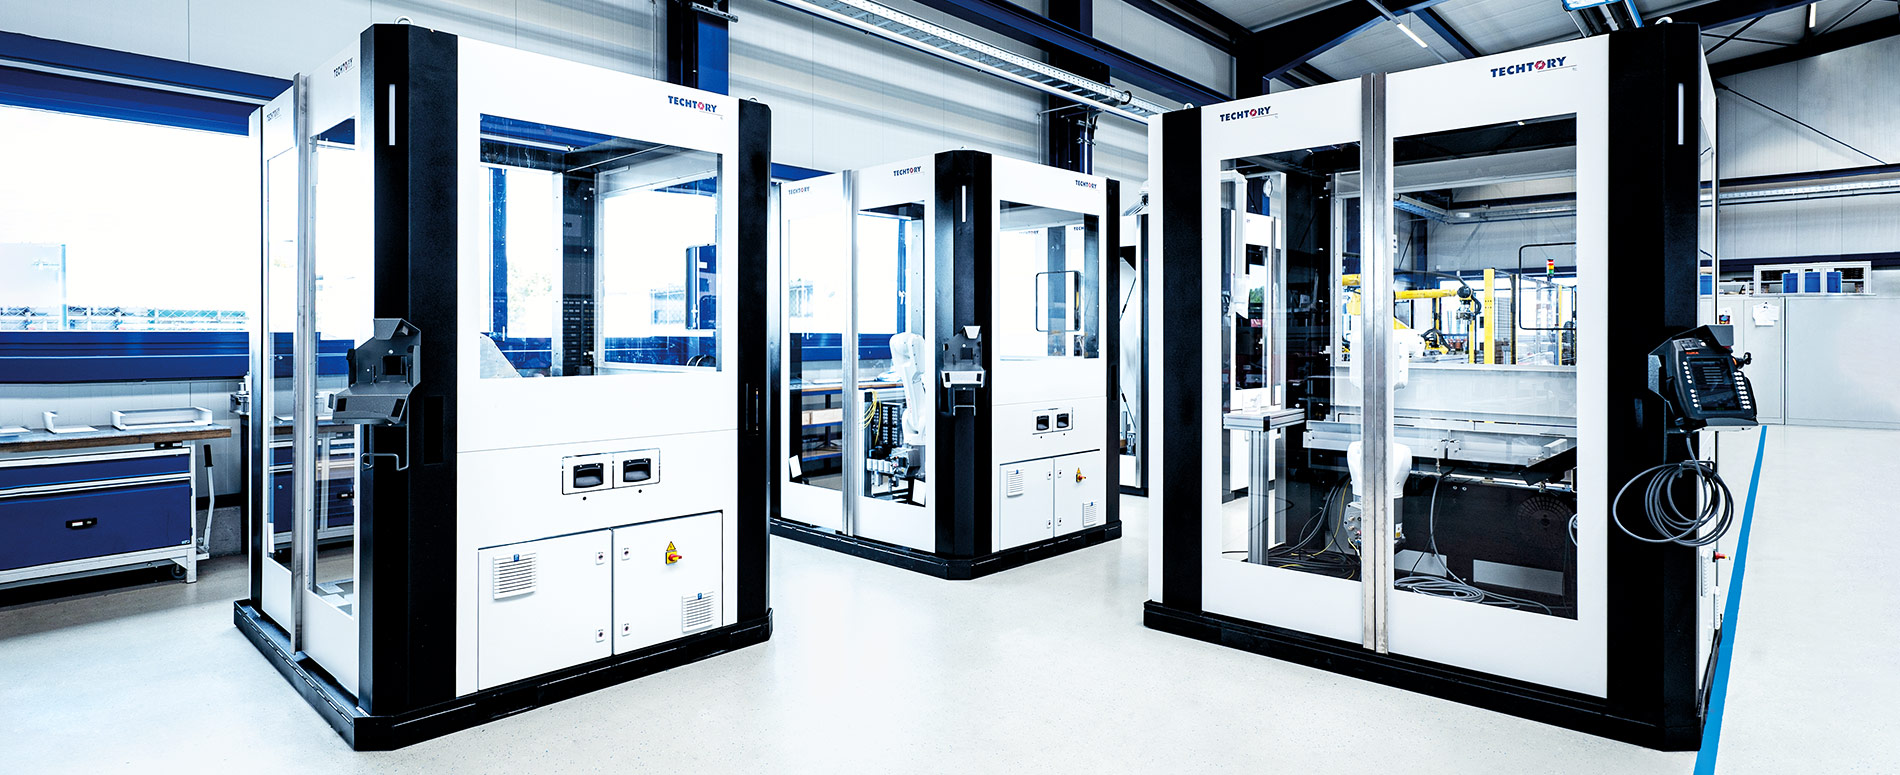
The system is based on the TECHTORY standard cell system and combines the advantages of the two cell types table-cell and floor-cell.
The workpieces are fed manually as bulk material into a vibratory conveyor system and separated by means of linear handling. Before the sliding blocks are transferred to the rotary indexing table, the holes are checked for presence, position and dirt using a vision sensor. This is followed by transfer to the individual processing stations. In stations 2+3, the threaded holes are deburred from the outside using countersinks and from the inside using brushes. Lances and nozzles in station 4 blow out the holes. In station 5, the sliding blocks are embossed with the part number and the company logo. A removal handling system then places the finished parts on a pivoting conveyor belt. This is used to fill three shipping cartons according to a previously defined quantity.
In a fully automated system, previously assembled ball valve housing units are stamped and tested for internal and external leaks in a leak testing station. Good parts are marked using a laser process, reject parts are ejected. Four leak test stations are installed in parallel to increase the cycle time.
After subsequent, fully automatic O-ring assembly, the presence and correct fit of the O-rings are monitored with a camera inspection. Good parts are marked by means of pad printing, reject parts are ejected.
A modular design and conversion kits make it possible to convert to different variants in a short space of time.
At an adjacent, semi-automated workstation for the manual assembly of small parts, the housing units are completed and packed with various small parts to form finished assemblies. The workstation is ergonomically designed and height-adjustable.
The equipment is built on the standard TECHTORY-table-cell. The insertion area, protected by safety light grids, is ergonomically designed. After manual oiling of the housing and insertion of various O-rings and plastic clips, these are clocked onward by means of a rotary indexing table to the camera inspection and press-fit station. The press-fit process is force-displacement monitored. A linear transfer handling system takes over the clocked onward transport. After renewed oiling and alignment, a functional test is carried out with camera monitoring. In further stations, the joined couplings are leak tested and labeled. Good parts are collected in a bag under the platform, n.o.k. parts are discharged via a chute.
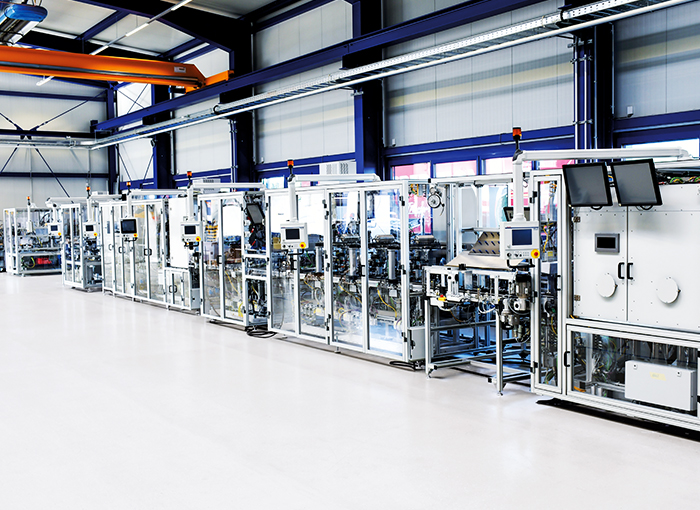
A complete, fully automatic production line for the assembly of electric coolant pumps was manufactured, assembled and commissioned on behalf of the customer.
Functions: soldering, optical solder joint inspection, housing cover feeding and fitting, laser welding, electronic PI testing, leak testing, laser marking.
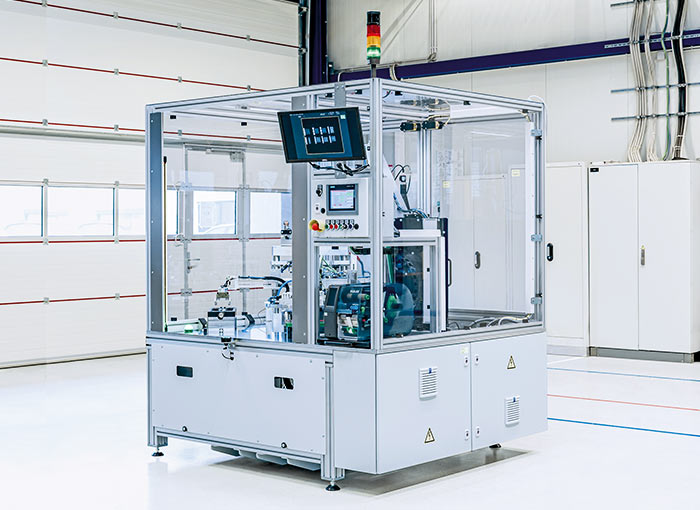
In a semi-automated assembly and testing system, the previously manually loaded injection molded parts are manually inserted into mold fixtures with automatic part scanning.
The indexing to the assembly station and then to the test station takes place via a rotary indexing table. The press-fit process is monitored for displacement and pressure.
A camera station checks the light guides for presence and the entire component for defects. The removal of the components is detected by a light barrier. A label is then output.
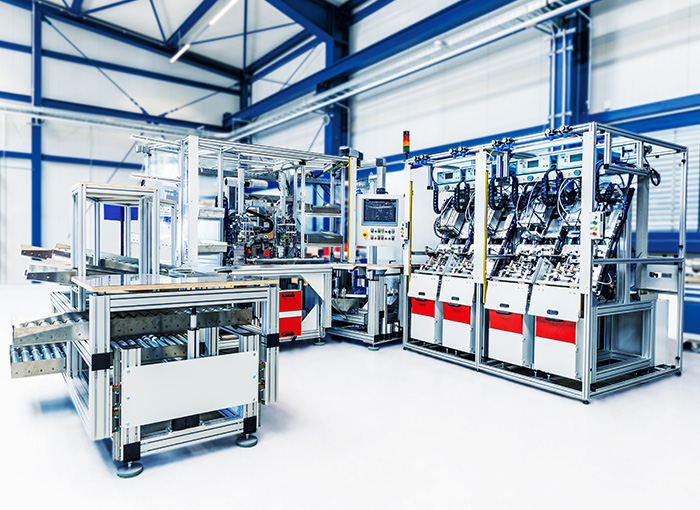
Ergonomic height-adjustable workstations were installed for the final testing of various components. Changeover devices with quick couplings for electrics and pneumatics allow flexible use for different products. A touch panel with visualization facilitates the operation.
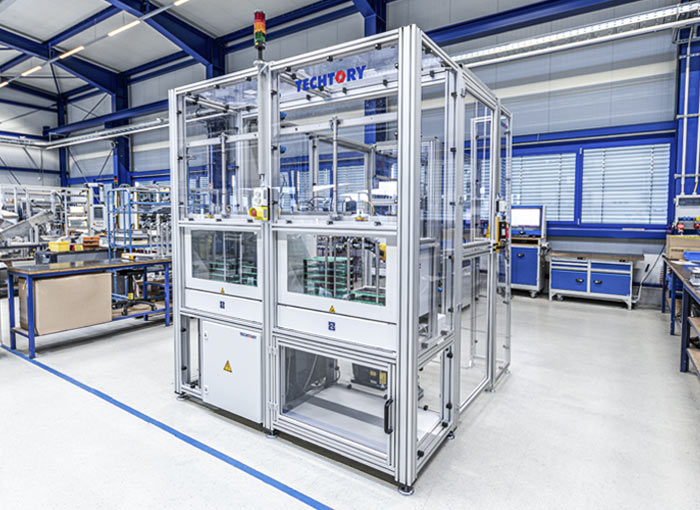
In a robotic cell, the entire machining process runs fully automatically.
A robot removes the films one by one before correcting the position supported by a camera and placing the films in a press.
The punched films are removed from the press by an independent linear handling system and deposited in another stacking box. Loading and unloading are carried out by the operator via drawer magazines.
The production process inside the cell is not disturbed by manual removal.

Efficient parts inspection every second is achieved through fully automated inspection of various criteria. The inspection of several features was realized in a space-saving way in a rotary indexing machine with 12 stations.
A visualization application with the WinCC flexible system was created for the clear mapping of all control processes.
The facility can be completely operated and monitored via the visualization. All the important process information, fault messages, facility parameters, etc. are displayed – operating errors can thus be avoided.

Automation and cutting technology
TECHTORY Automation GmbH
Ludwig-Winter-Straße 5
77767 Appenweier
| Phone | +49 7805 9589-0 |
| Fax: | +49 7805 9589-50 |
| Email: | info@techtory.de |